

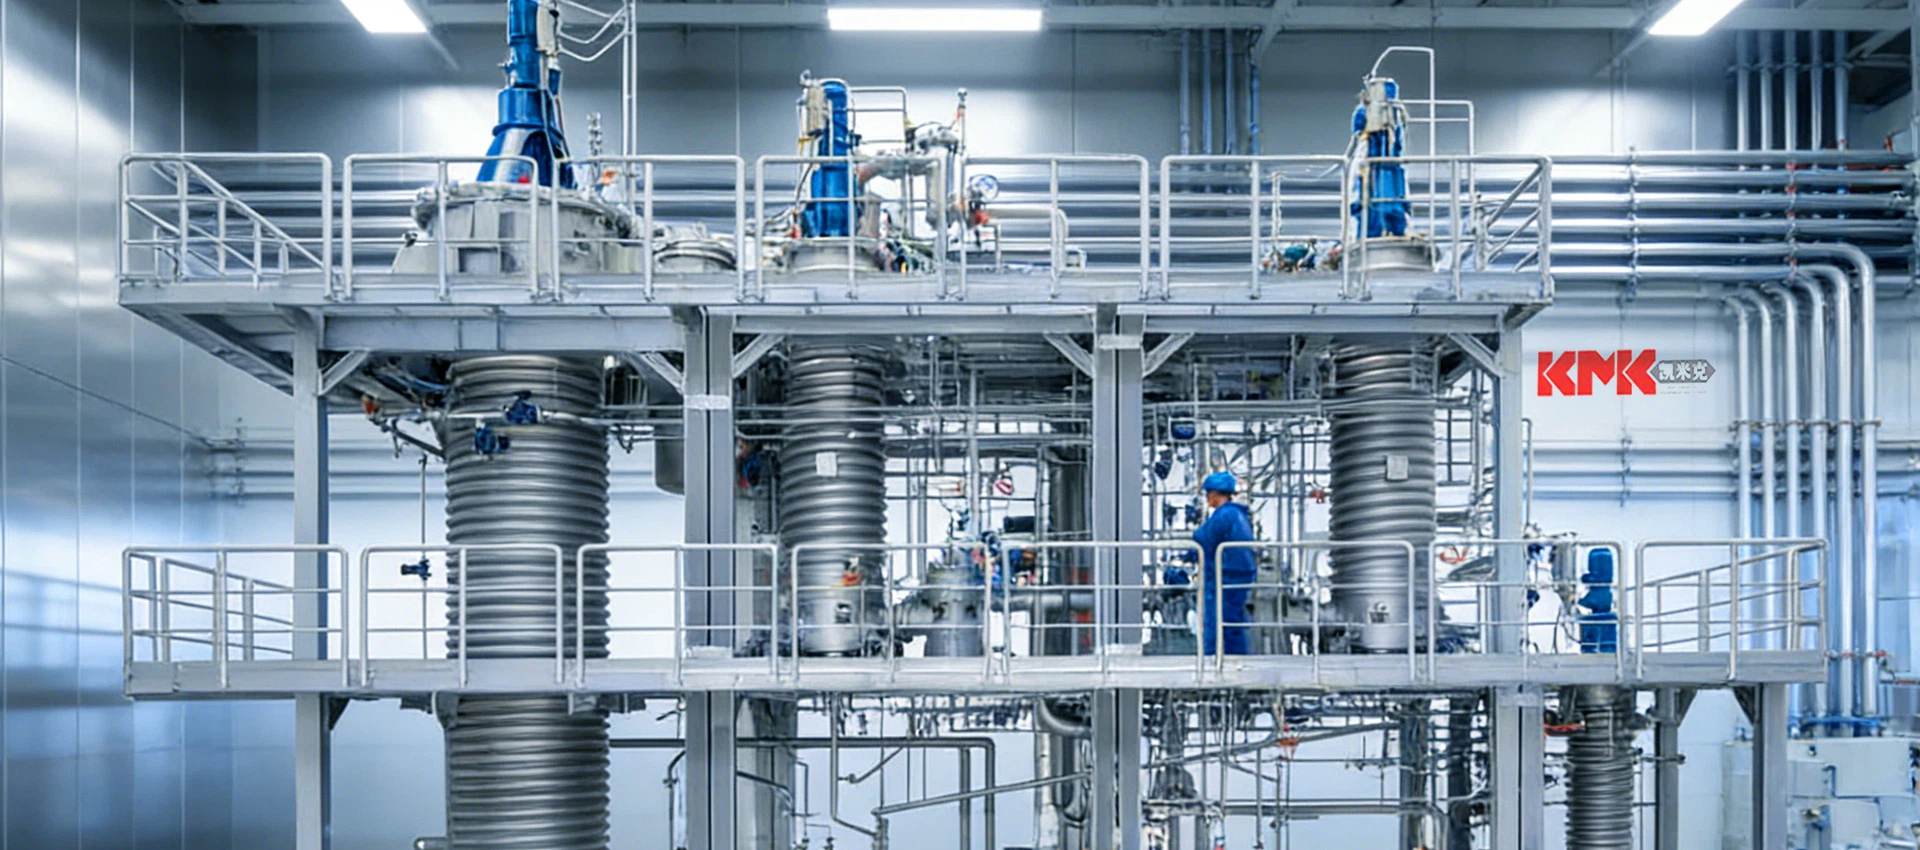


Stainless Steel Industrial Heat Exchanger
Description
Technical Parameters
Our stainless steel industrial heat exchangers adopt premium 304, 304L and 316L stainless steel materials and precision manufacturing. Designed for complex industrial scenarios with high temperature, high pressure and corrosive environments, the equipment delivers stable heat transfer, outstanding durability and efficient energy-saving performance in full-range industrial heat exchange operations.
Effectively solving traditional equipment's pain points such as rusting, corrosion, low efficiency and frequent maintenance, our stainless steel heat exchangers support liquid, gas and multi-phase medium heat exchange and waste heat recovery. Optimized flow channel design greatly improves heat transfer efficiency, reduces energy consumption and lowers overall operating costs.

Product Features
High Efficiency & Energy Saving: Optimized flow channel and structure expand effective heat transfer area, realizing fast and uniform heat exchange, reducing heat loss and achieving energy-efficient production.
Corrosion Resistance & Durability: Made of industrial and food-grade stainless steel, the equipment resists oxidation, rust and medium corrosion. It withstands frequent temperature and pressure changes for long-term stable service.
Wide Compatibility: Applicable for water, oil, chemical solvents, gas and other media. It supports high/low temperature heating, constant temperature control and waste heat recovery for diverse industrial processes.
Customizable Structure: Available in shell-and-tube, plate, finned tube and U-tube types. Custom non-standard designs are offered to match specific pressure, temperature and flow requirements.
Low Maintenance: Smooth stainless steel surface prevents scaling and blockage. Easy to clean and maintain, it minimizes downtime and ensures continuous production.
Stable & Safe Operation: Precision welding and rigorous pressure-bearing structure ensure zero-leakage operation under alternating high and low pressure and temperature, meeting strict industrial standards.

Product Applications
Widely applied in chemical, petrochemical, power generation, HVAC, food & beverage, pharmaceutical, seawater cooling, new energy, sewage treatment and waste heat recovery industries.

Why Choose Our Stainless Steel Heat Exchangers?
All stainless steel heat exchangers are manufactured under strict pressure vessel standards with professional welding, pressure testing and non-destructive inspection, ensuring reliable and consistent quality.
We provide standard and customized solutions for conventional and special working conditions. Compared with carbon steel equipment, stainless steel heat exchangers feature higher cleanliness, stronger corrosion resistance, longer service life and lower maintenance costs, ideal for clean and harsh industrial environments.
Suitable for constant temperature heating, cooling, waste heat recovery and sterile heat exchange processes, our stainless steel heat exchangers provide efficient, safe and energy-saving thermal solutions for industrial production.


Hot Tags
Stainless steel heat exchanger, stainless steel industrial heat exchanger, stainless steel shell and tube heat exchanger, stainless steel plate heat exchanger, stainless steel U-tube heat exchanger, stainless steel finned tube heat exchanger, corrosion resistant heat exchanger, food grade heat exchanger, pharmaceutical sterile heat exchanger, China stainless steel heat exchanger manufacturer, supplier, factory
Hot Tags: stainless steel industrial heat exchanger, China stainless steel industrial heat exchanger manufacturers, suppliers, factory, ASME Certified Titanium Heat Exchangers, ASME U Stamped Heat Exchanger, Baffle Heat Exchanger, Cross Flow Heat Exchanger, Heat Exchanger Equipment, Titanium Shell Tube Heat Exchangers
Previous
No InformationNext
Vacuum Paddle DryerSend Inquiry


