

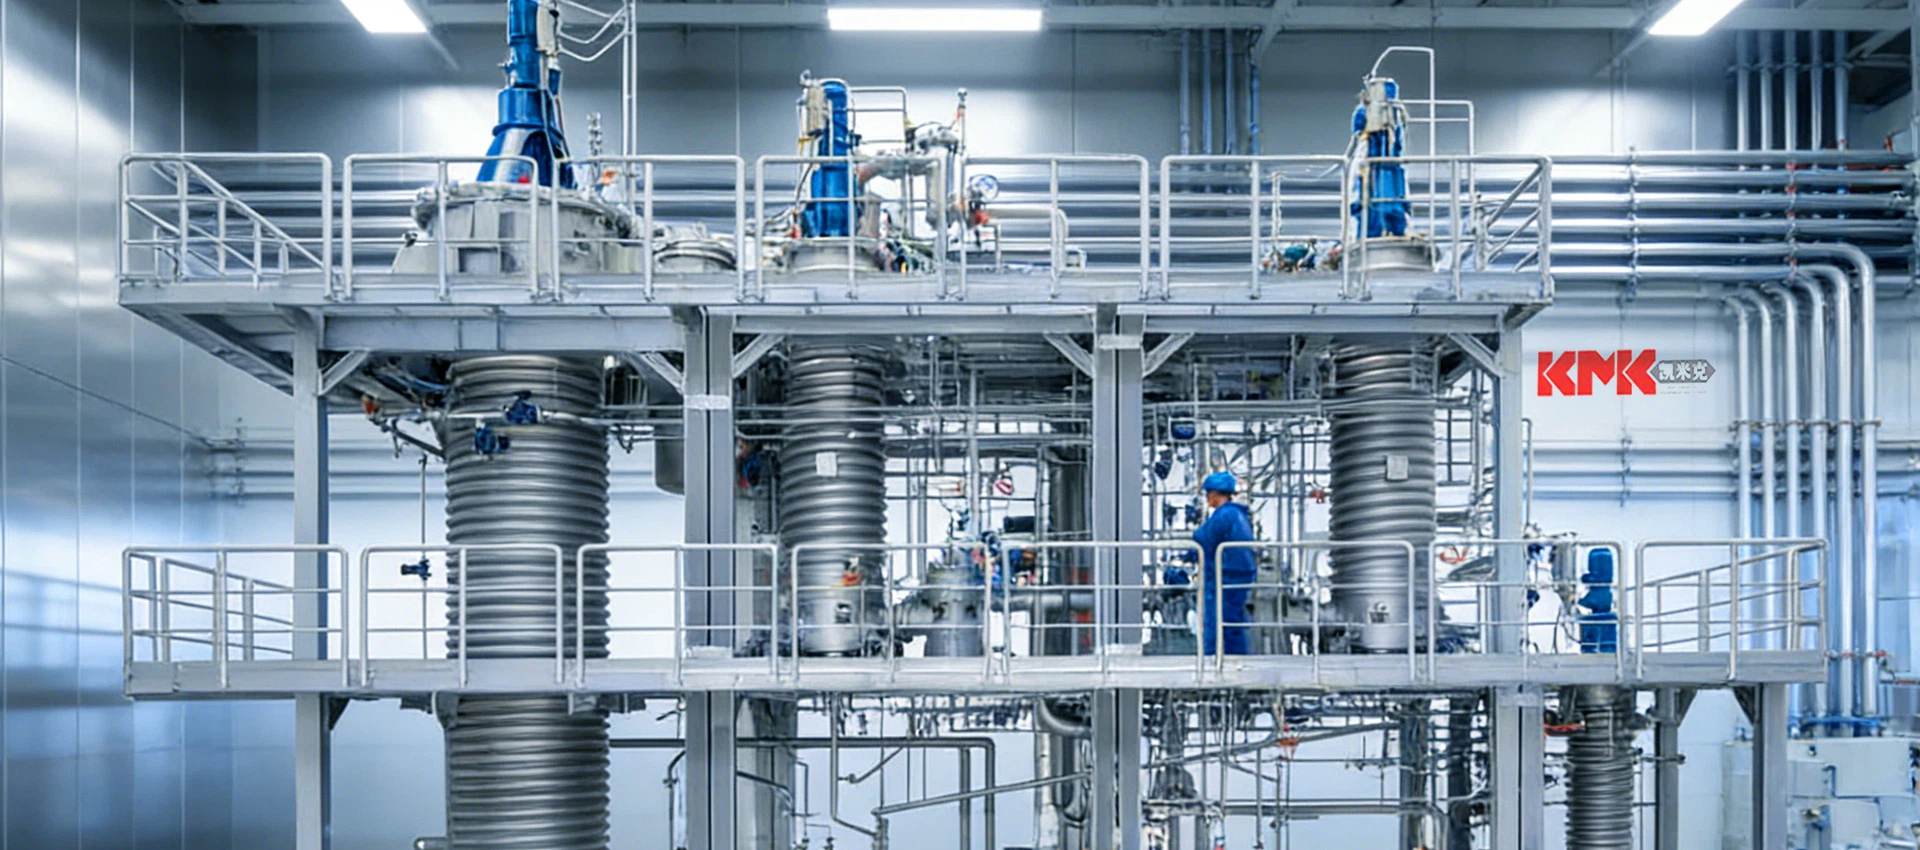

Gas-Liquid Heat Exchanger
Description
Technical Parameters
Our gas-liquid heat exchangers are widely used for industrial gas and liquid heat exchange. Adopting turbulent tube bundle structure, they deliver stable and efficient heat transfer with anti-scaling, energy-saving, space-saving, pressure-resistant and corrosion-resistant performance, ideal for petrochemical, power, HVAC, pharmaceutical and environmental protection industries.
Core Functions
1. High Heat Transfer Efficiency: Professionally designed gas-liquid flow channels ensure full medium contact and uniform heat exchange, suitable for continuous high-flow and high-load production.
2. Excellent Energy Saving: High waste heat recovery rate greatly reduces heat loss, helping enterprises cut operating energy costs by over 30%.
3. Space-saving Compact Design: Modular integrated structure saves more than 35% floor space compared with traditional models, fitting narrow workshop environments.
4. Strong Pressure & Corrosion Resistance: Available in 304, 316L, carbon steel, titanium and other materials, the sturdy structure adapts to complex working conditions with slight corrosion.
5. Intelligent Management: Optional IoT monitoring system tracks real-time temperature, pressure and heat transfer status, optimizing operation for longer and more stable service life.

Typical Applications
1. Petrochemical Industry: Process gas cooling, liquid preheating, reactor temperature control and tail gas waste heat recovery.
2. Power & Energy: Generator waste heat recovery, gas system heat exchange and industrial waste heat reuse.
3. Food & Pharmaceutical: Fermentation tank temperature control, medium heating and cooling, production heat recycling.
4. HVAC System: District heating, central air conditioning heat exchange and unit constant temperature control.
5. Environmental Protection: Flue gas cooling, sewage treatment temperature control and waste gas heat recovery.
Innovative Design
• Optimized Heat Transfer Structure: Multi-stage turbulent tube bundles optimize gas-liquid flow speed for more uniform and efficient heat exchange.
• Anti-blocking & Anti-scaling Performance: Large-flow polished channels prevent dust and scale buildup, supporting long-term stable operation.
• Pressure Stabilization Design: Reinforced pressure-bearing structure resists pressure fluctuation, reduces equipment loss and ensures stable operation.
Quality Certification
Manufactured in full compliance with pressure vessel standards, our heat exchangers are certified with ASME BPVC, PED, CE and ISO 9001, delivering reliable quality for domestic and international industrial projects.


Hot Tags: gas-liquid heat exchanger, China gas-liquid heat exchanger manufacturers, suppliers, factory, ASME Certified Storage Tank Fabrication, chemical storage product provider, chemical storage standard, Electric Heating Reaction Kettle, Stainless Steel Storage Tank Pressure Vessel ASME Tank, Titanium alloy medicine tank
Previous
No InformationSend Inquiry


