

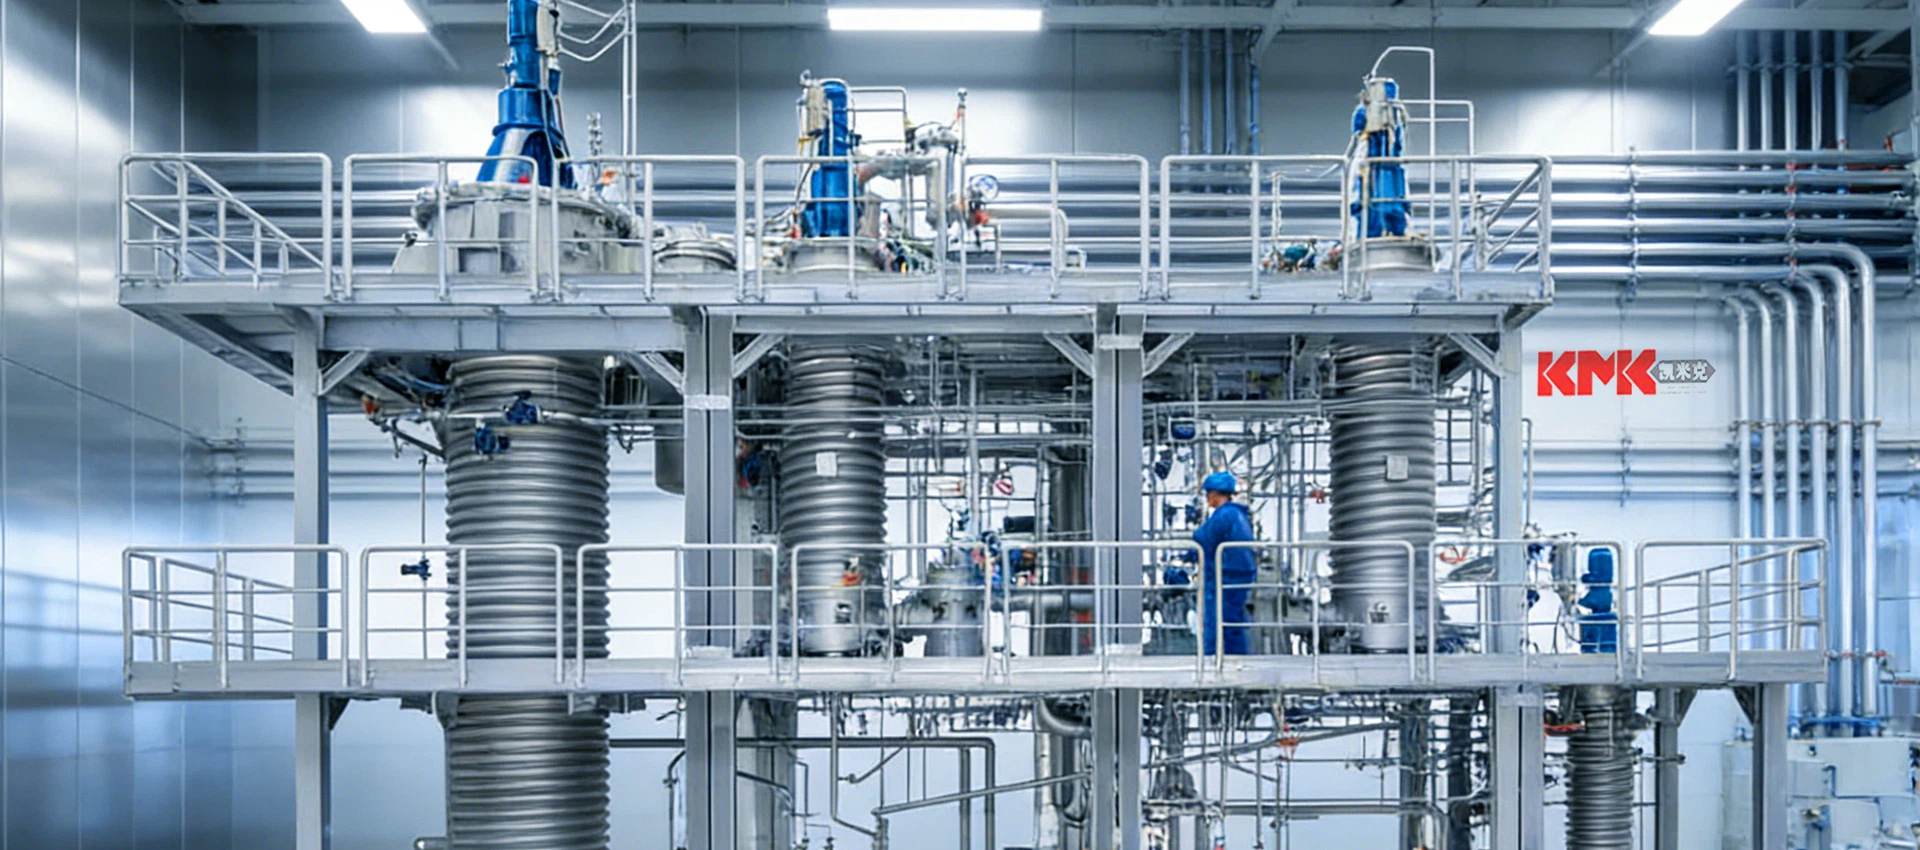

Distillation Column Tower
Description
Technical Parameters
Distillation towers are core industrial equipment that utilize the differences in boiling points between components of a mixture to separate and purify them through a vaporization-condensation cycle. They are widely used in the petroleum, chemical, and pharmaceutical industries. Distillation towers offer high separation efficiency, strong adaptability, and continuous and stable operation. They also control energy consumption through waste heat recovery and are easily controlled with automated systems.
Advantages and Features
- High Separation Efficiency: The Column Distillation Tower achieves high-purity separations exceeding 99.9%, meeting stringent purity requirements in applications such as fine chemicals and pharmaceuticals.
- Adaptability: The Stainless Steel Ethanol Distillation Tower can process a wide range of materials, from low-carbon hydrocarbons to high-boiling-point organics, adapting to diverse separation needs by adjusting tray/packing type and operating parameters.
- Continuous and Stable Operation: The continuous feed-discharge design allows for 24-hour uninterrupted operation, ensuring continuous industrial production.
- Controllable Energy Consumption: Combined with waste heat recovery and heat pump systems, it effectively reduces energy consumption, meeting energy conservation and environmental protection requirements.
- Easy Operation and Control: The Copper Distillation Tower utilizes automated control systems for liquid level, temperature, and pressure, enabling precise adjustment of separation efficiency and reducing manual intervention costs.

Application Areas
Petrochemical Industry: Separating crude oil into fractions such as gasoline, diesel, and kerosene, or purifying petrochemical raw materials such as ethylene and propylene;
Chemical Industry: Purifying products during the production of solvents such as ethanol and methanol, or separating chemical intermediates such as acetic acid and benzene;
Pharmaceutical Industry: Purifying pharmaceutical raw materials and intermediates, such as separating organic solvents in antibiotic production to ensure drug purity;
Food Industry
Distillation Column Towers are used in alcohol distillation, fruit juice concentration, and purification of food additives;
Environmental Protection
Treating industrial wastewater and recovering organic solvents to achieve resource recycling and meet emission standards.

834M
Total Freelancer
732M
Positive Review
90M
Order recieved
236M
Projects Completed
why choose us
A high-tech enterprise specializing in the research, development, design and manufacturing of chemical equipment such as reaction equipment, distillation equipment, evaporation equipment, crystallization equipment, etc.
With years of industry experience and technological innovation, KMK equipment engineers focus on designing chemical equipment such as reaction, distillation, evaporation, and crystallization, which are widely used in petrochemical, pharmaceutical, fine chemical, food, biology, oil, flavor, environmental protection and other industries.
As a leading manufacturer of chemical equipment such as reaction equipment, distillation equipment, evaporation equipment, crystallization equipment, we are committed to providing customers with efficient, reliable and durable fine chemical equipment solutions.
Our company has a 200 square meter laboratory and can provide small-scale test equipment such as distillation towers, scraped film evaporation, molecular distillation, gas stripping, drying, crystallization, etc. After years of research and development, design, manufacturing and engineering system integration, we have accumulated considerable experience and have now developed into a professional company that provides one-stop services such as research and development design, manufacturing, installation, instrument automation, commissioning, and training.


Hot Tags: distillation column tower, China distillation column tower manufacturers, suppliers, factory, Molecular distillation pilot plant, chemical distillation unit, durable distillation unit, pressure distillation unit, Automatic Distillation Apparatus, Crosslik agent TAIC Production Equipment
Send Inquiry


